Article Content
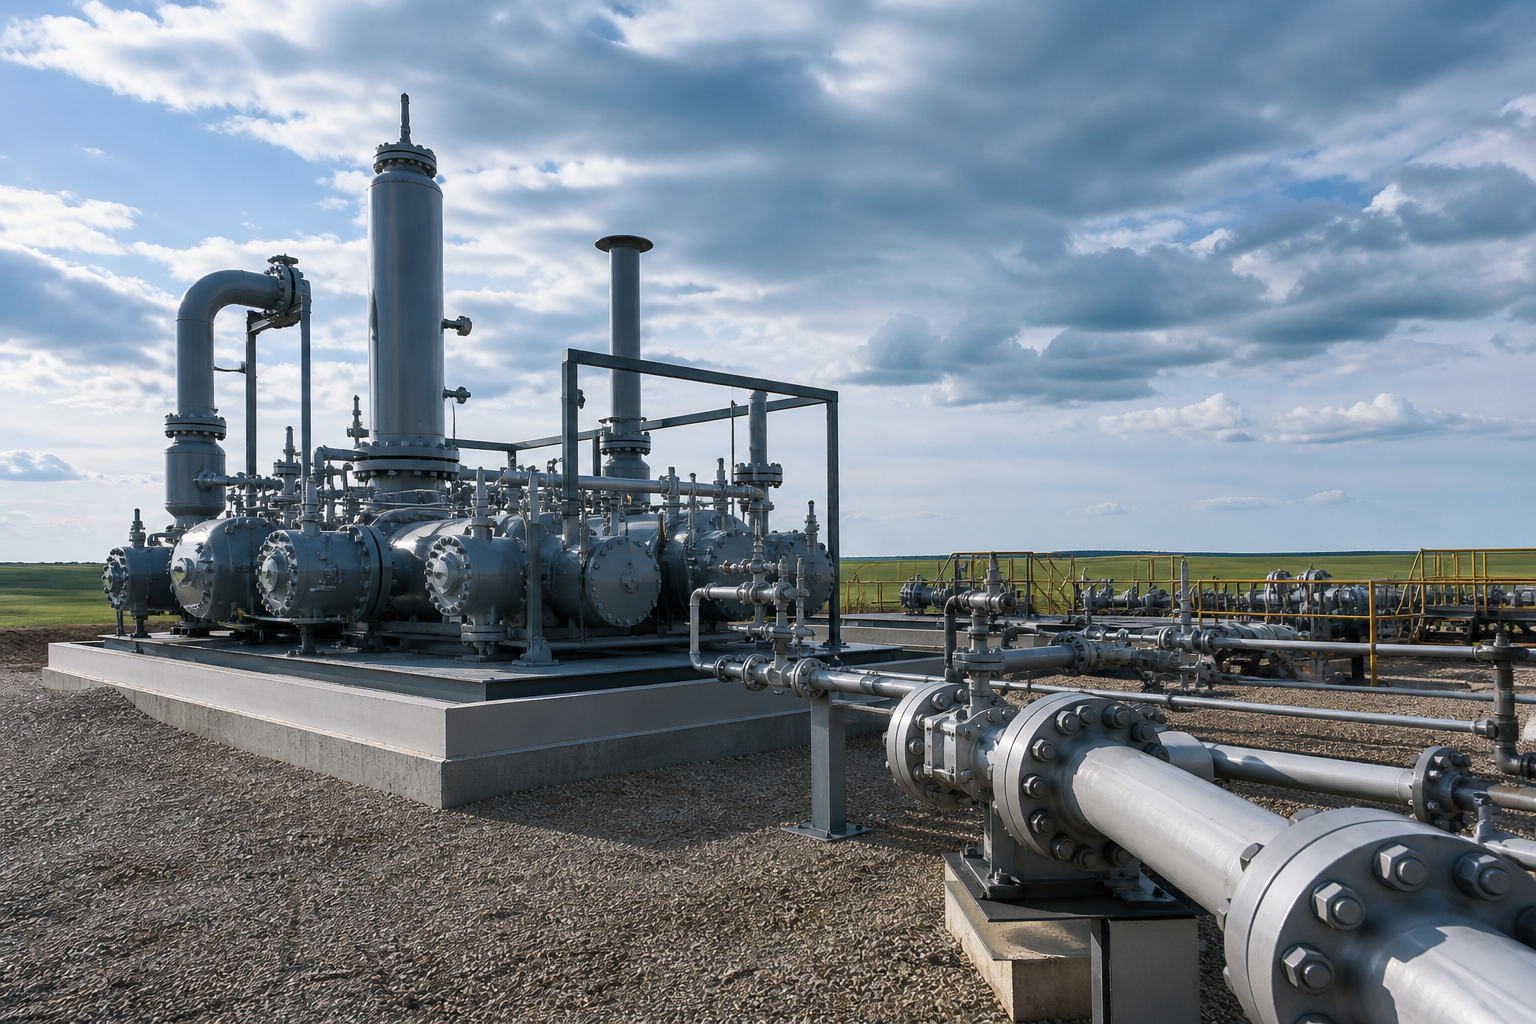
Acid gas injection for H2S is a disposal pathway that compresses concentrated hydrogen sulfide (and usually carbon dioxide) from a gas sweetening unit and injects it into a suitable subsurface formation. For many mid-size sour gas plants, upgraders, and remote facilities, it sits between two extremes: building a full Claus sulfur recovery unit with tail-gas treating, or relying indefinitely on non-regenerable scavengers and adsorbents. This article is an unbiased engineering overview of when acid gas injection makes sense, what the process train requires, and how operators should frame reservoir, compression, integrity, and safety decisions before committing CAPEX.
When Acid Gas Injection Makes Sense
Claus sulfur recovery remains the default for large, continuous H2S loads where elemental sulfur has a market or where regulations expect high sulfur recovery efficiency. Acid gas injection becomes attractive when:
- Sulfur rate is modest Illustrative plant ranges often discussed in industry screening are on the order of a few tonnes per day of sulfur equivalent rather than tens of tonnes; always size from measured acid-gas composition and flow, not from a brochure average.
- Sulfur markets are weak or logistics are poor Remote pads may face high trucking costs for liquid sulfur or limited offtake, eroding the value of an SRU byproduct.
- CAPEX and complexity of Claus + TGTU do not pay back Tail-gas treating, incineration, and SO2 limits can dominate economics for smaller plants.
- A competent disposal reservoir exists — Porosity, permeability, containment seals, and regulatory acceptance are prerequisites, not afterthoughts.
- CO2 co-injection is acceptable or desirable — Many amine acid-gas streams are H2S/CO2 mixtures; AGI can dispose of both without a separate CO2 vent strategy.
- Temporary scavenger spend is climbing — Sites that bridged with liquid scavengers or solid beds for years sometimes re-evaluate AGI once sustained sulfur load is proven.
AGI is not a shortcut around gas sweetening. You still need reliable H2S removal from the sales-gas or fuel-gas path; AGI only answers what happens to the concentrated acid gas after the amine (or equivalent) regenerator.
How an AGI Train Typically Fits Together
A typical acid gas injection for H2S flowsheet includes:
- Gas sweetening Amine or another regenerable solvent produces a rich acid-gas overhead from the regenerator.
- Knockout and cooling — Remove free liquids; manage water and hydrocarbon carryover that would damage compressors or form hydrates.
- Compression Multi-stage compression raises acid gas to injection pressure. Interstage cooling and liquid knockout are critical.
- Dehydration / conditioning Control water dewpoint to protect against hydrates and corrosion; some designs add further polishing for hydrocarbons or oxygen.
- Pipeline or flowline to the well — Materials, leak detection, and isolation philosophy must match sour, high-pressure service.
- Injection well and reservoir — Designed for continuous or campaign injection with monitoring of pressure, rate, and annulus integrity.
Hybrid sites may still use scavengers or mobile scrubbers for upset bypass, start-up, or low-rate wells that never justify tying into the AGI header. The decision is rarely AGI or nothing; it is what is permanent bulk disposal versus what remains polishing or contingency.”
Reservoir and Well Considerations
Subsurface performance decides whether AGI is viable long term. Engineering due diligence usually covers:
- Containment — Caprock integrity, faulting, and offset wellbore pathways that could allow migration toward usable aquifers or surface.
- Injectivity Can the formation accept the design rate at allowable bottomhole pressure without fracturing outside the approved zone?
- Fluid compatibility H2S/CO2/water mixtures can dissolve carbonate rock, precipitate scales, or mobilize fines; lab and analog studies reduce surprises.
- Pressure management Cumulative inventory, plume size, and pressure interference with nearby producers or injectors.
- Well metallurgy and completion Sour-service tubulars, packers, and wellhead equipment selected for H2S partial pressure and water wetness (NACE/ISO sour-service practice as applicable).
- Monitoring wells and MMV — Pressure gauges, annulus monitoring, and a measurement, monitoring, and verification plan proportional to risk and regulatory expectations.
Illustrative caution: an injectivity test on sweet water or CO2-only fluid does not automatically prove performance with wet H2S-rich acid gas. Design the appraisal program around the real injectate.
Compression, Dehydration, and Materials Challenges
Acid gas is not “just another compressor gas.” Common field pain points include:
- Corrosion — Wet H2S and CO2 drive general corrosion, sulfide stress cracking risk in susceptible materials, and iron sulfide fouling.
- Hydrates Water plus acid gas under pressure forms hydrates readily; temperature control, glycol or molecular-sieve dehydration, and methanol contingency plans matter.
- Elemental sulfur and solids Temperature and pressure swings can drop sulfur or other solids in coolers, scrubbers, and valves.
- Hydrocarbon carryover — Liquid hydrocarbons from poor knockout foul compressors and change reservoir behavior.
- Oxygen ingress — Small air leaks in low-pressure sections can worsen corrosion and sulfur chemistry.
- Seal and packing life Sour gas compressors need maintenance philosophies that assume aggressive service, not sweet-gas intervals.
Metallurgy and elastomer selection should follow a documented materials philosophy for each pressure stagenot a single sour grade everywhere” assumption that ignores temperature, water, and chlorides.
Comparing AGI, Claus/SRU, and Scavenging
| Factor | Acid gas injection | Claus SRU + tail-gas treating | Liquid scavengers / solid adsorbents |
|---|---|---|---|
| Best when | Sustained acid-gas rate + proven disposal reservoir | Large continuous sulfur load + sulfur offtake or strict recovery rules | Low rate, intermittent, or temporary duty |
| Product / fate of sulfur | Remains underground as acid gas | Elemental sulfur (plus residual emissions management) | Spent chemical or spent media waste |
| CAPEX profile | Compression, pipeline, well, MMV | High (thermal/catalytic stages, TGTU, incineration) | Low equipment; higher consumable OPEX |
| OPEX drivers | Power, compression maintenance, well/reservoir surveillance | Fuel/steam, catalysts, sulfur handling, emissions compliance | Chemistry/media + disposal logistics |
| Key technical risk | Reservoir containment and injectivity | Reliability of SRU/TGTU and SO2 limits | Breakthrough, solids, waste classification |
| Flexibility | Tied to reservoir capacity and approved rates | Plant-centric; hard to turn down economically | Easy to scale up/down or mobilize |
Use the table as a screening frame. A site with rising scavenger bills and a nearby depleted zone may screen toward AGI; a high-LTPD gas plant with existing sulfur logistics usually screens toward Claus.
Monitoring, Integrity, and Regulatory Themes
Jurisdictions differ, but AGI projects typically face expectations around:
- Approved disposal zone and maximum pressures
- Well integrity (tubing, casing, cement, annulus pressure)
- Leak detection on surface piping and wellhead
- Emergency shut-in and flare/vent philosophy for compressor trips
- Public safety planning for H2S release scenarios
- Reporting of injection volumes, pressures, and incidents
Western Canadian operators often align designs with provincial energy-regulator frameworks for sour gas and injection schemes. Do not copy another provinces well file as a template—match the local application package, setbacks, and emergency-planning zone methodology. Treat regulatory engagement as a critical path item equal to compressor lead time.
Safety and Operating Discipline
Concentrated H2S streams demand plant-level discipline even when the product” never reaches a sulfur pit:
- Fixed and portable H2S detection around compressors, coolers, knockout drums, and the wellhead
- Breathing apparatus and rescue plans for confined or congested work
- Isolation, purging, and blinding procedures for compressor maintenance
- Clear ESD hierarchy: what trips injection, what holds inventory, what flares safely under permit
- Drills that include pipeline rupture and wellhead leak scenarios, not only amine-unit upsets
- Contractor control—wireline, well servicing, and compressor overhauls introduce people unfamiliar with the AGI layout
AGI moves hazard from an SRU sulfur fire or SO2 stack problem into a high-pressure toxic inventory problem. The hazard is different, not smaller.
Economics: What Actually Moves the Needle
Rough order-of-magnitude thinking (illustrative only) usually hinges on:
- Power cost for multi-stage compression
- Availability (unplanned compressor downtime that forces flaring, scavenging, or production cuts)
- Well workovers and surveillance over the project life
- Avoided SRU CAPEX and TGTU complexity
- Avoided scavenger and disposal spend relative to continuing non-regenerable treating
- Carbon and emissions accounting if CO2 would otherwise be vented or if sulfur plant incineration dominates local air permits
A lifecycle cost comparison should include the cost of failure modes: lost injectivity, a replacement well, or a forced return to scavengers during a multi-month compressor rebuild. Cheap AGI on paper that cannot run 95% of the year is expensive in practice.
Operators sometimes underestimate the interface between AGI and the sweetening unit. Regenerator overhead composition swings with amine health, reboiler duty, and feed-gas H2S/CO2 ratio. An AGI compressor train sized on a single steady-state heat-and-material balance can struggle when the regenerator runs rich after a feed spike or lean after a turnaround. Include design margins for composition and molecular weight, and agree in advance what happens to acid gas when compression is unavailable: permitted flare, temporary scavenger contactor, production curtailment, or a combination.
Another recurring gap is water accounting across the whole train. Water enters with the acid gas from the regenerator, from knockout efficiency limits, and from any wash or antifoulant programs. That water must leave somehowas knockout liquids, as glycol-rich streams, or as vapor that still meets a hydrate-safe dewpoint at the coldest expected metal temperature. A dehydration package that looks adequate in summer ambient conditions can be marginal in winter when aerial coolers run colder. Western Canadian winters make this a design case, not an operating note.
Limitations and Failure Modes
Acid gas injection for H2S is not appropriate when:
- No secure disposal formation is available within economic pipeline distance
- Acid-gas rate is so high that SRU economics clearly win and sulfur can be handled
- Reservoir pressure or plume constraints cap injection below plant needs
- Materials or water management problems make compression chronically unreliable
- Community, surface-rights, or regulatory barriers block approval on an acceptable schedule
- The acid gas” is too contaminated with oxygen, NOx, or liquids for reliable compression without major pre-treatment
Common operational failure modes include hydrate plugs after a cooldown, cooler fouling from sulfur, rising injection pressure from near-wellbore damage, and annulus pressure anomalies that force shut-in. Build spares, bypass, and contingency treating into the operating philosophy before first gas.
Conclusion
Acid gas injection for H2S is a proven mid-scale alternative when concentrated acid gas must be managed without a full Claus train—or when continuing scavenger and adsorbent spend no longer matches a stable sulfur load. Success depends on reservoir containment and injectivity, sour-service compression and dehydration design, materials integrity, regulatory alignment, and a safety program built for high-pressure toxic inventory. It complements, rather than replaces, disciplined gas sweetening and still leaves room for polishing scavengers, adsorbents, and mobile scrubbers during outages and low-rate edges of the system.
FirstKlaz Technologies supports operators with H2S scavengers and adsorbents, scrubber and bubble-column design, sulfur-recovery and treating evaluations, and RFP facilitation when comparing AGI, Claus, redox, and hybrid options. For an unbiased engineering discussion of an acid-gas disposal or sweetening path, contact info@fklaz.com.